Boiler and cooling tower systems require precise chemical dosing to prevent scale, corrosion, and microbiological growth that compromise efficiency and asset life. Blue-White® manufactures chemical metering pumps, flow meters, and integrated chemical feed skid systems designed for reliable performance in boiler water and cooling tower treatment applications. From oxygen scavengers and alkalinity control to biocides and scale inhibitors, our solutions help protect equipment, reduce energy loss, and optimize chemical consumption.
From coagulation and disinfection to metals removal and dechlorination, our solutions help operators maintain compliance, protect infrastructure, and optimize chemical usage.
Operational Compliance
Reliable Water Treatment For Boilers & Cooling Systems
Boilers and cooling systems are critical to industrial heating, power generation, and facility climate control. Improperly treated water leads to scale buildup, corrosion, fouling, and bacterial growth — all of which reduce heat transfer efficiency, increase fuel and energy costs, and shorten equipment life.
Effective chemical treatment supports:
Higher system efficiency and uptime
Extended equipment lifespan
Lower maintenance and chemical costs
Compliance with environmental and safety standards
Maintaining stable, accurately controlled dosing is essential to consistent system protection.
Treatment Applications
Common Chemical Applications
Boiler & Cooling Tower Water Treatment processes require accurate dosing for:
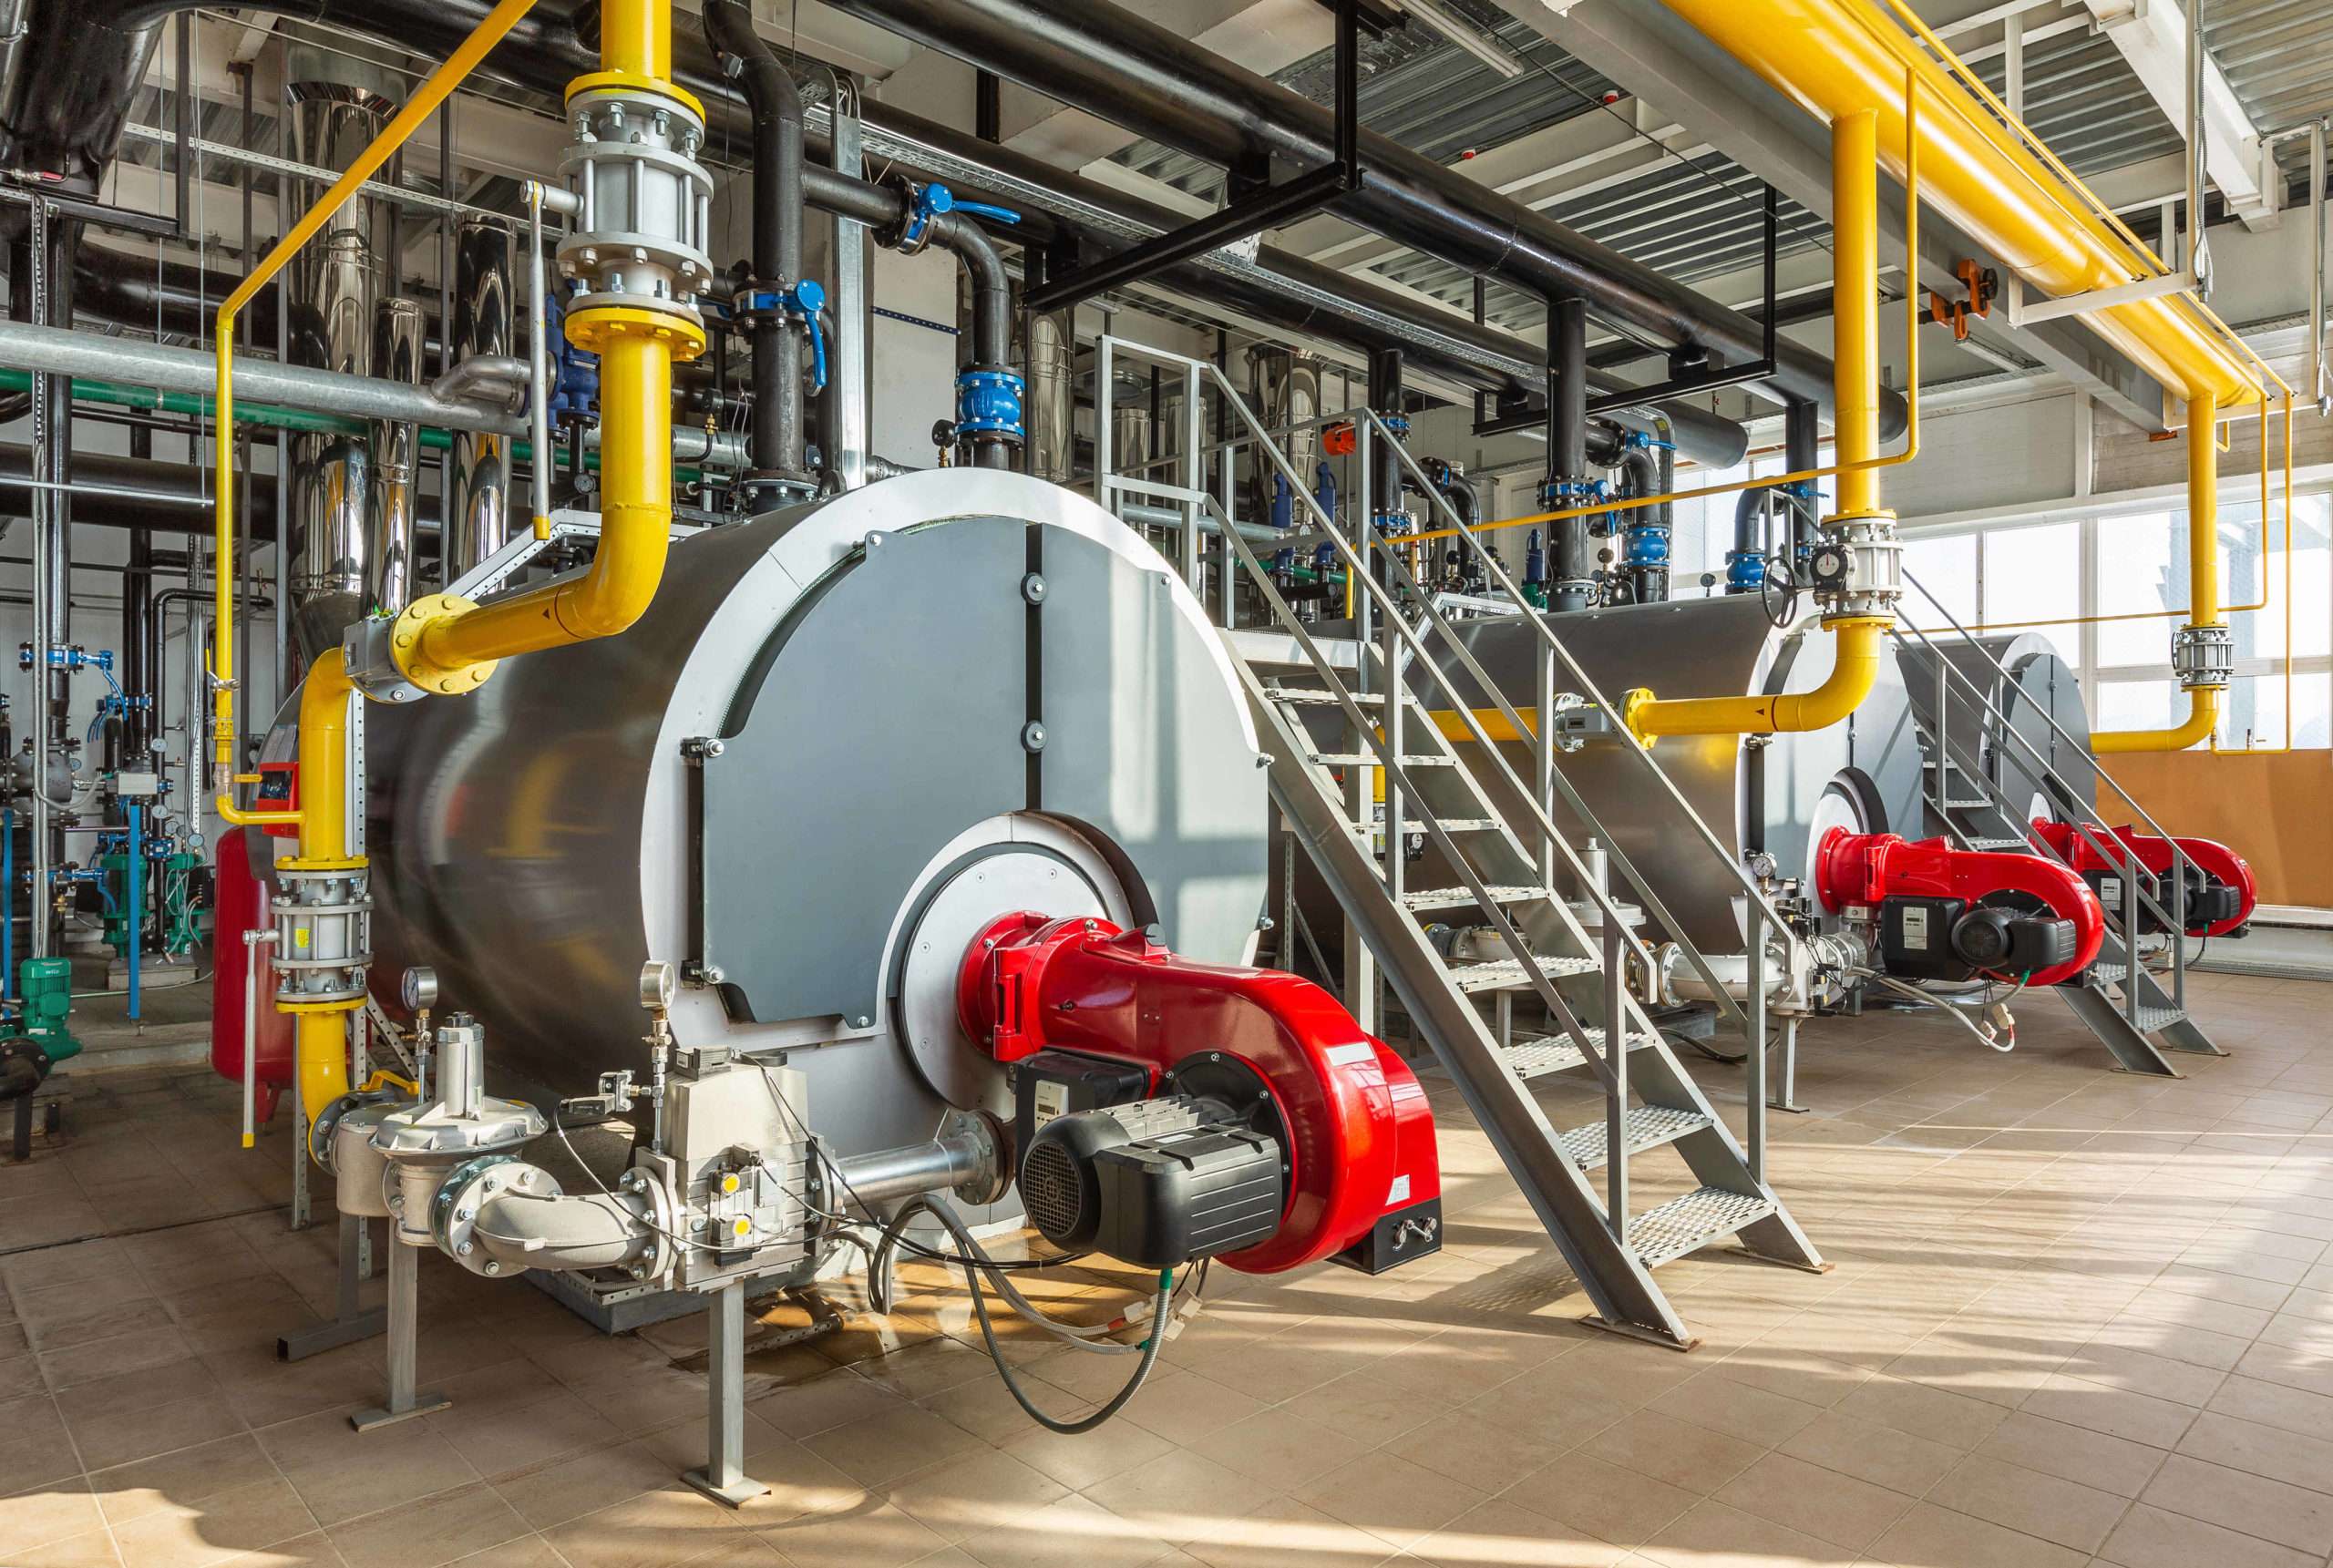
Boiler Water Treatment using oxygen scavengers, alkalinity builders, phosphates or polymers, anti-foaming agents, and amines to prevent corrosion, control scale, and protect condensate systems.
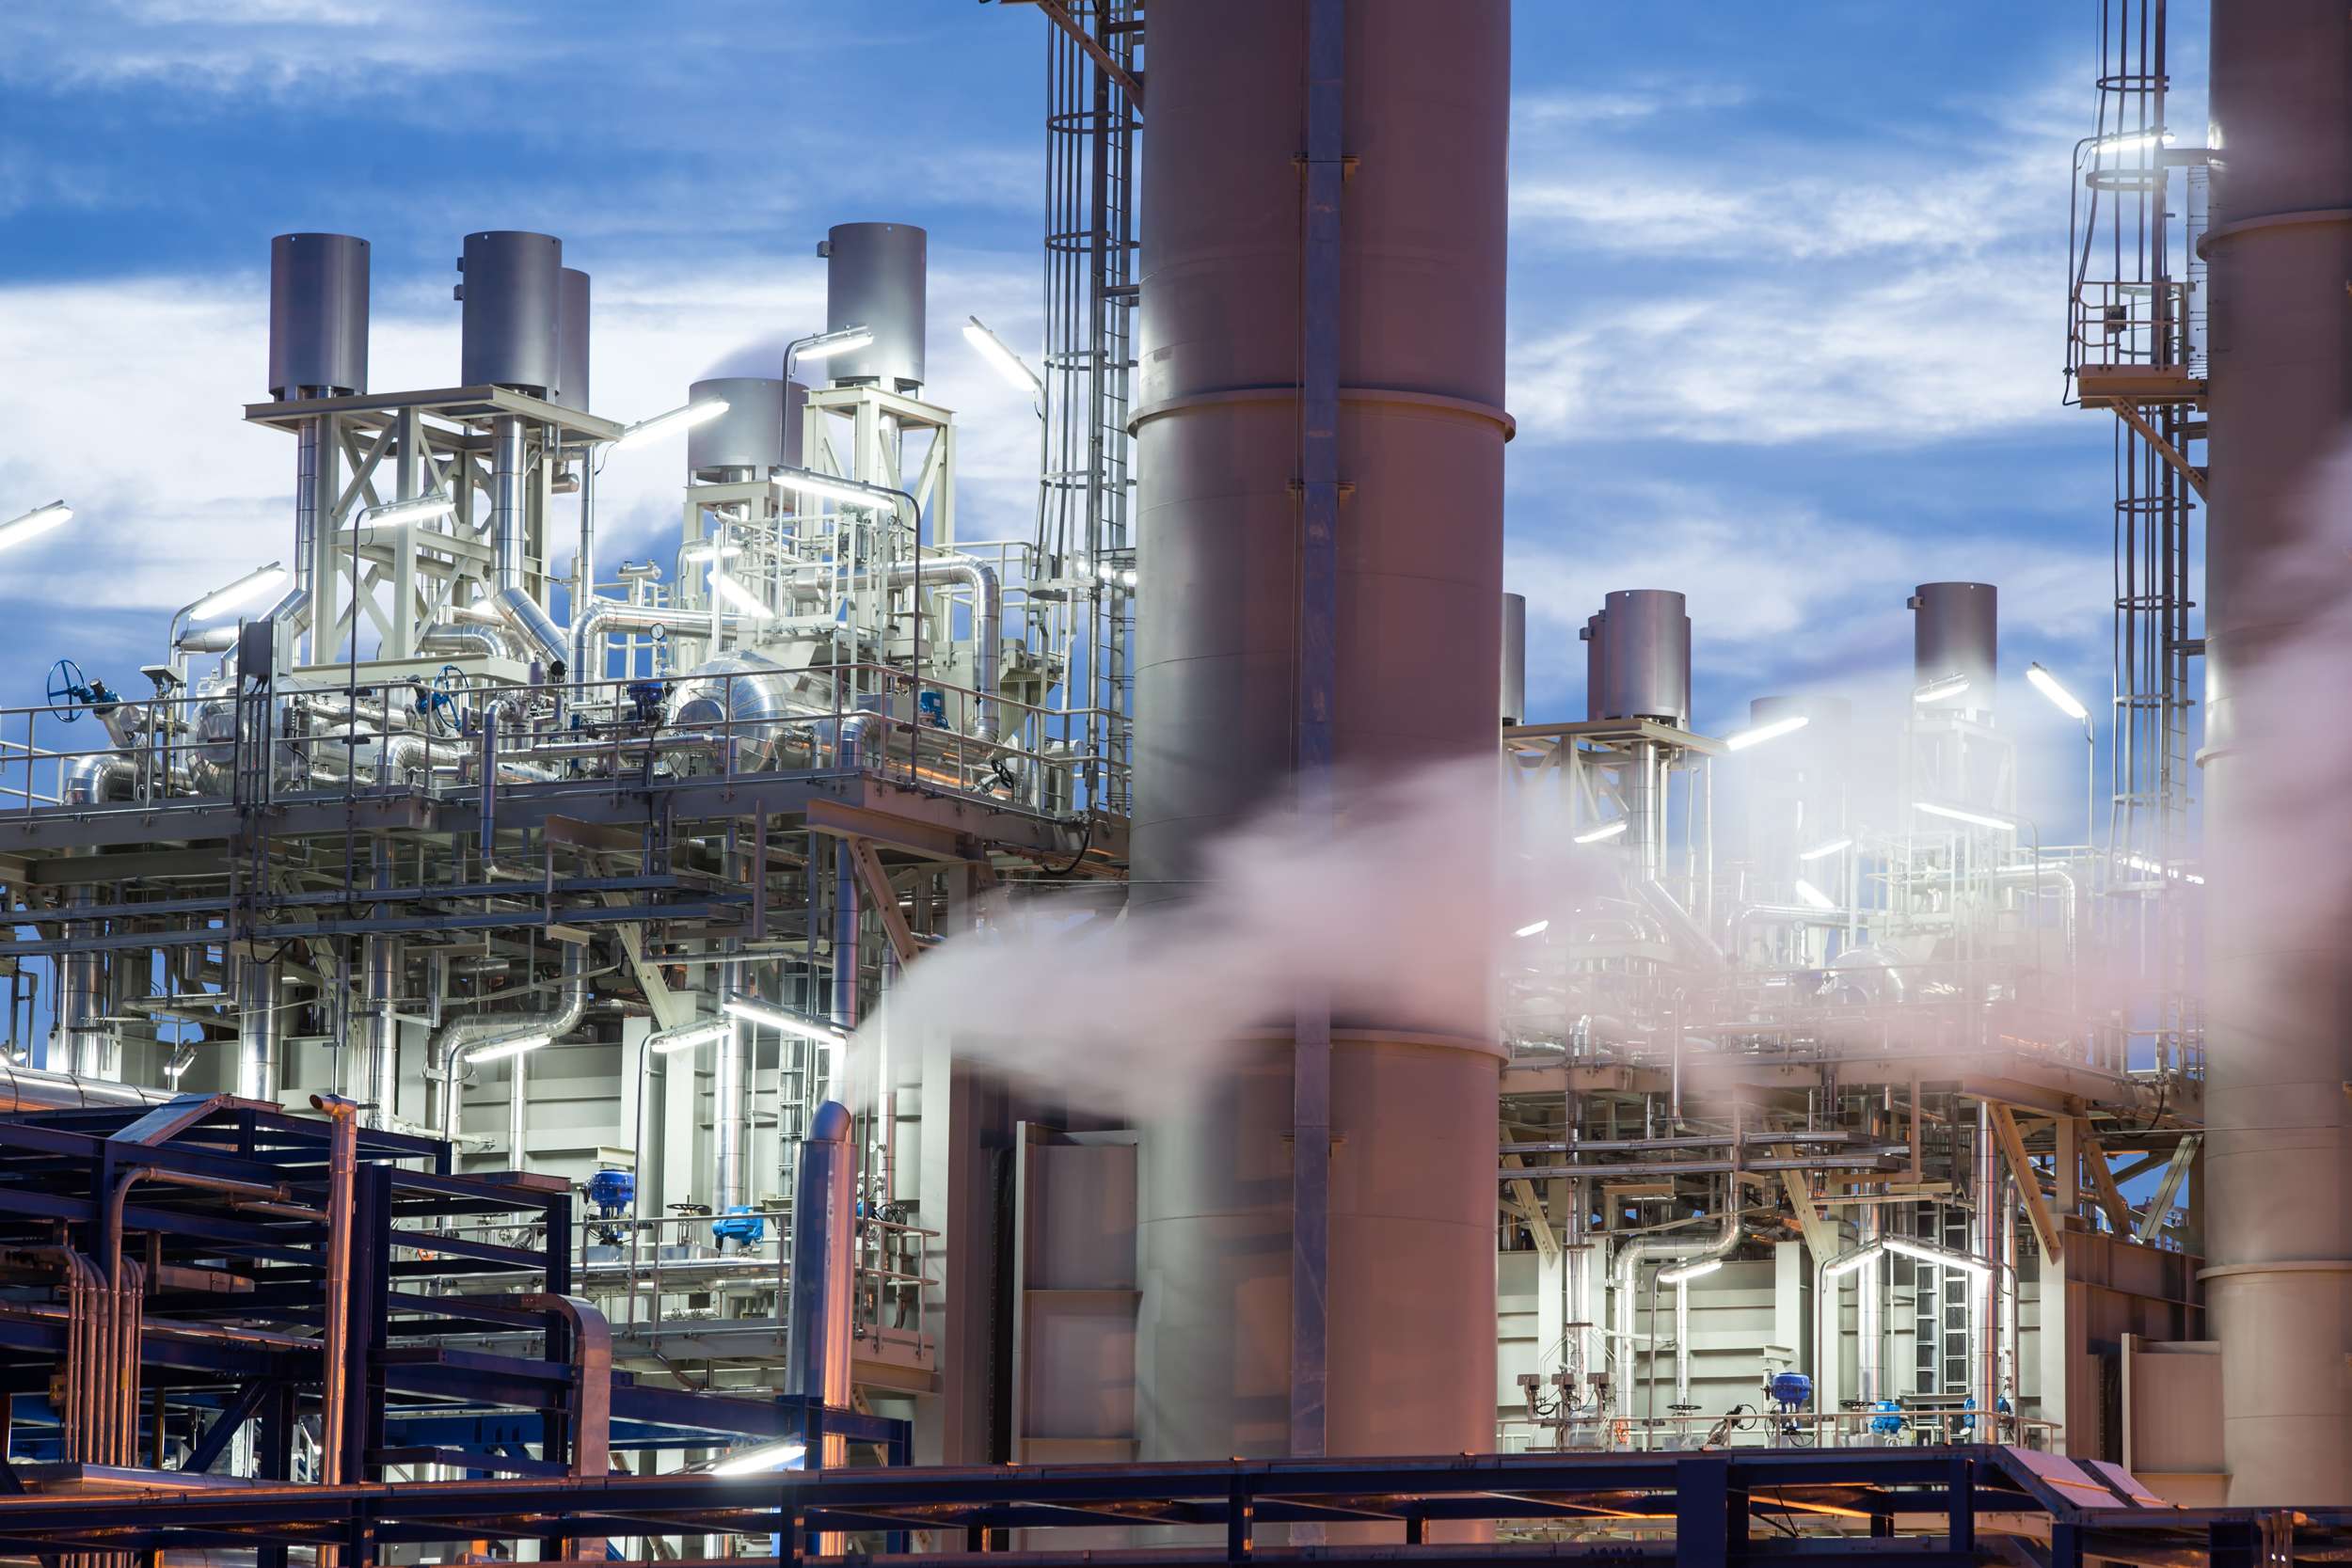
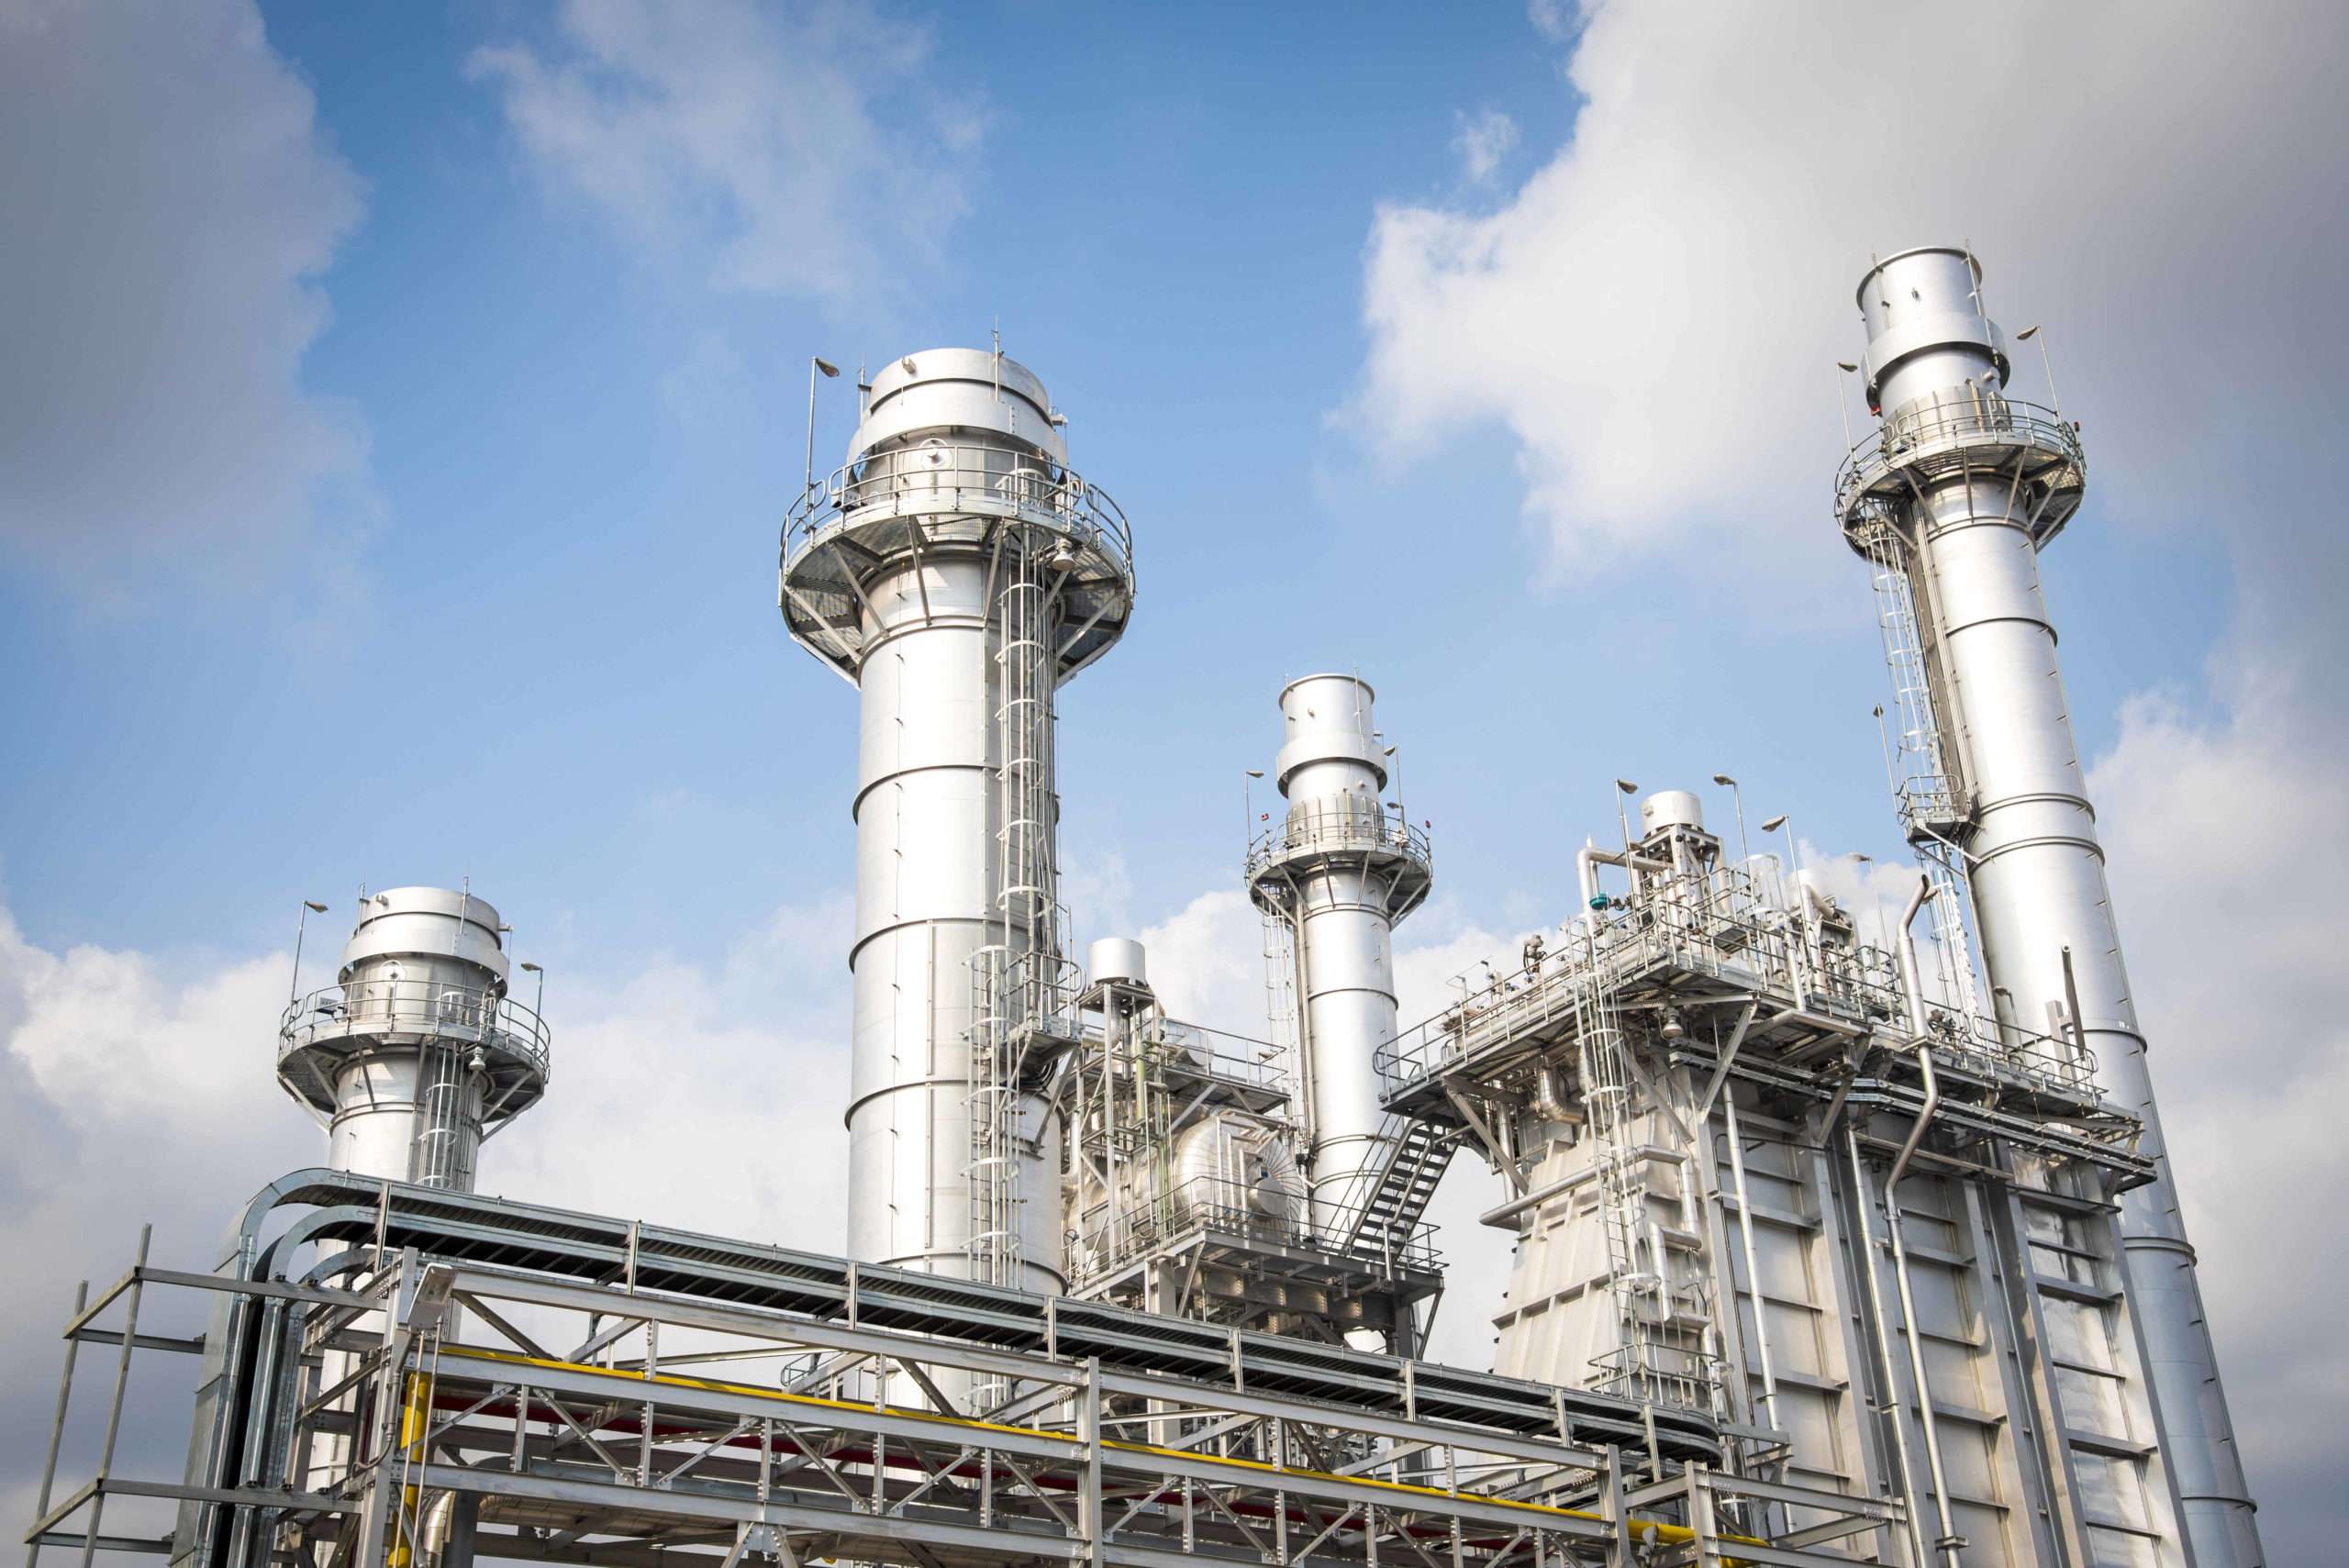
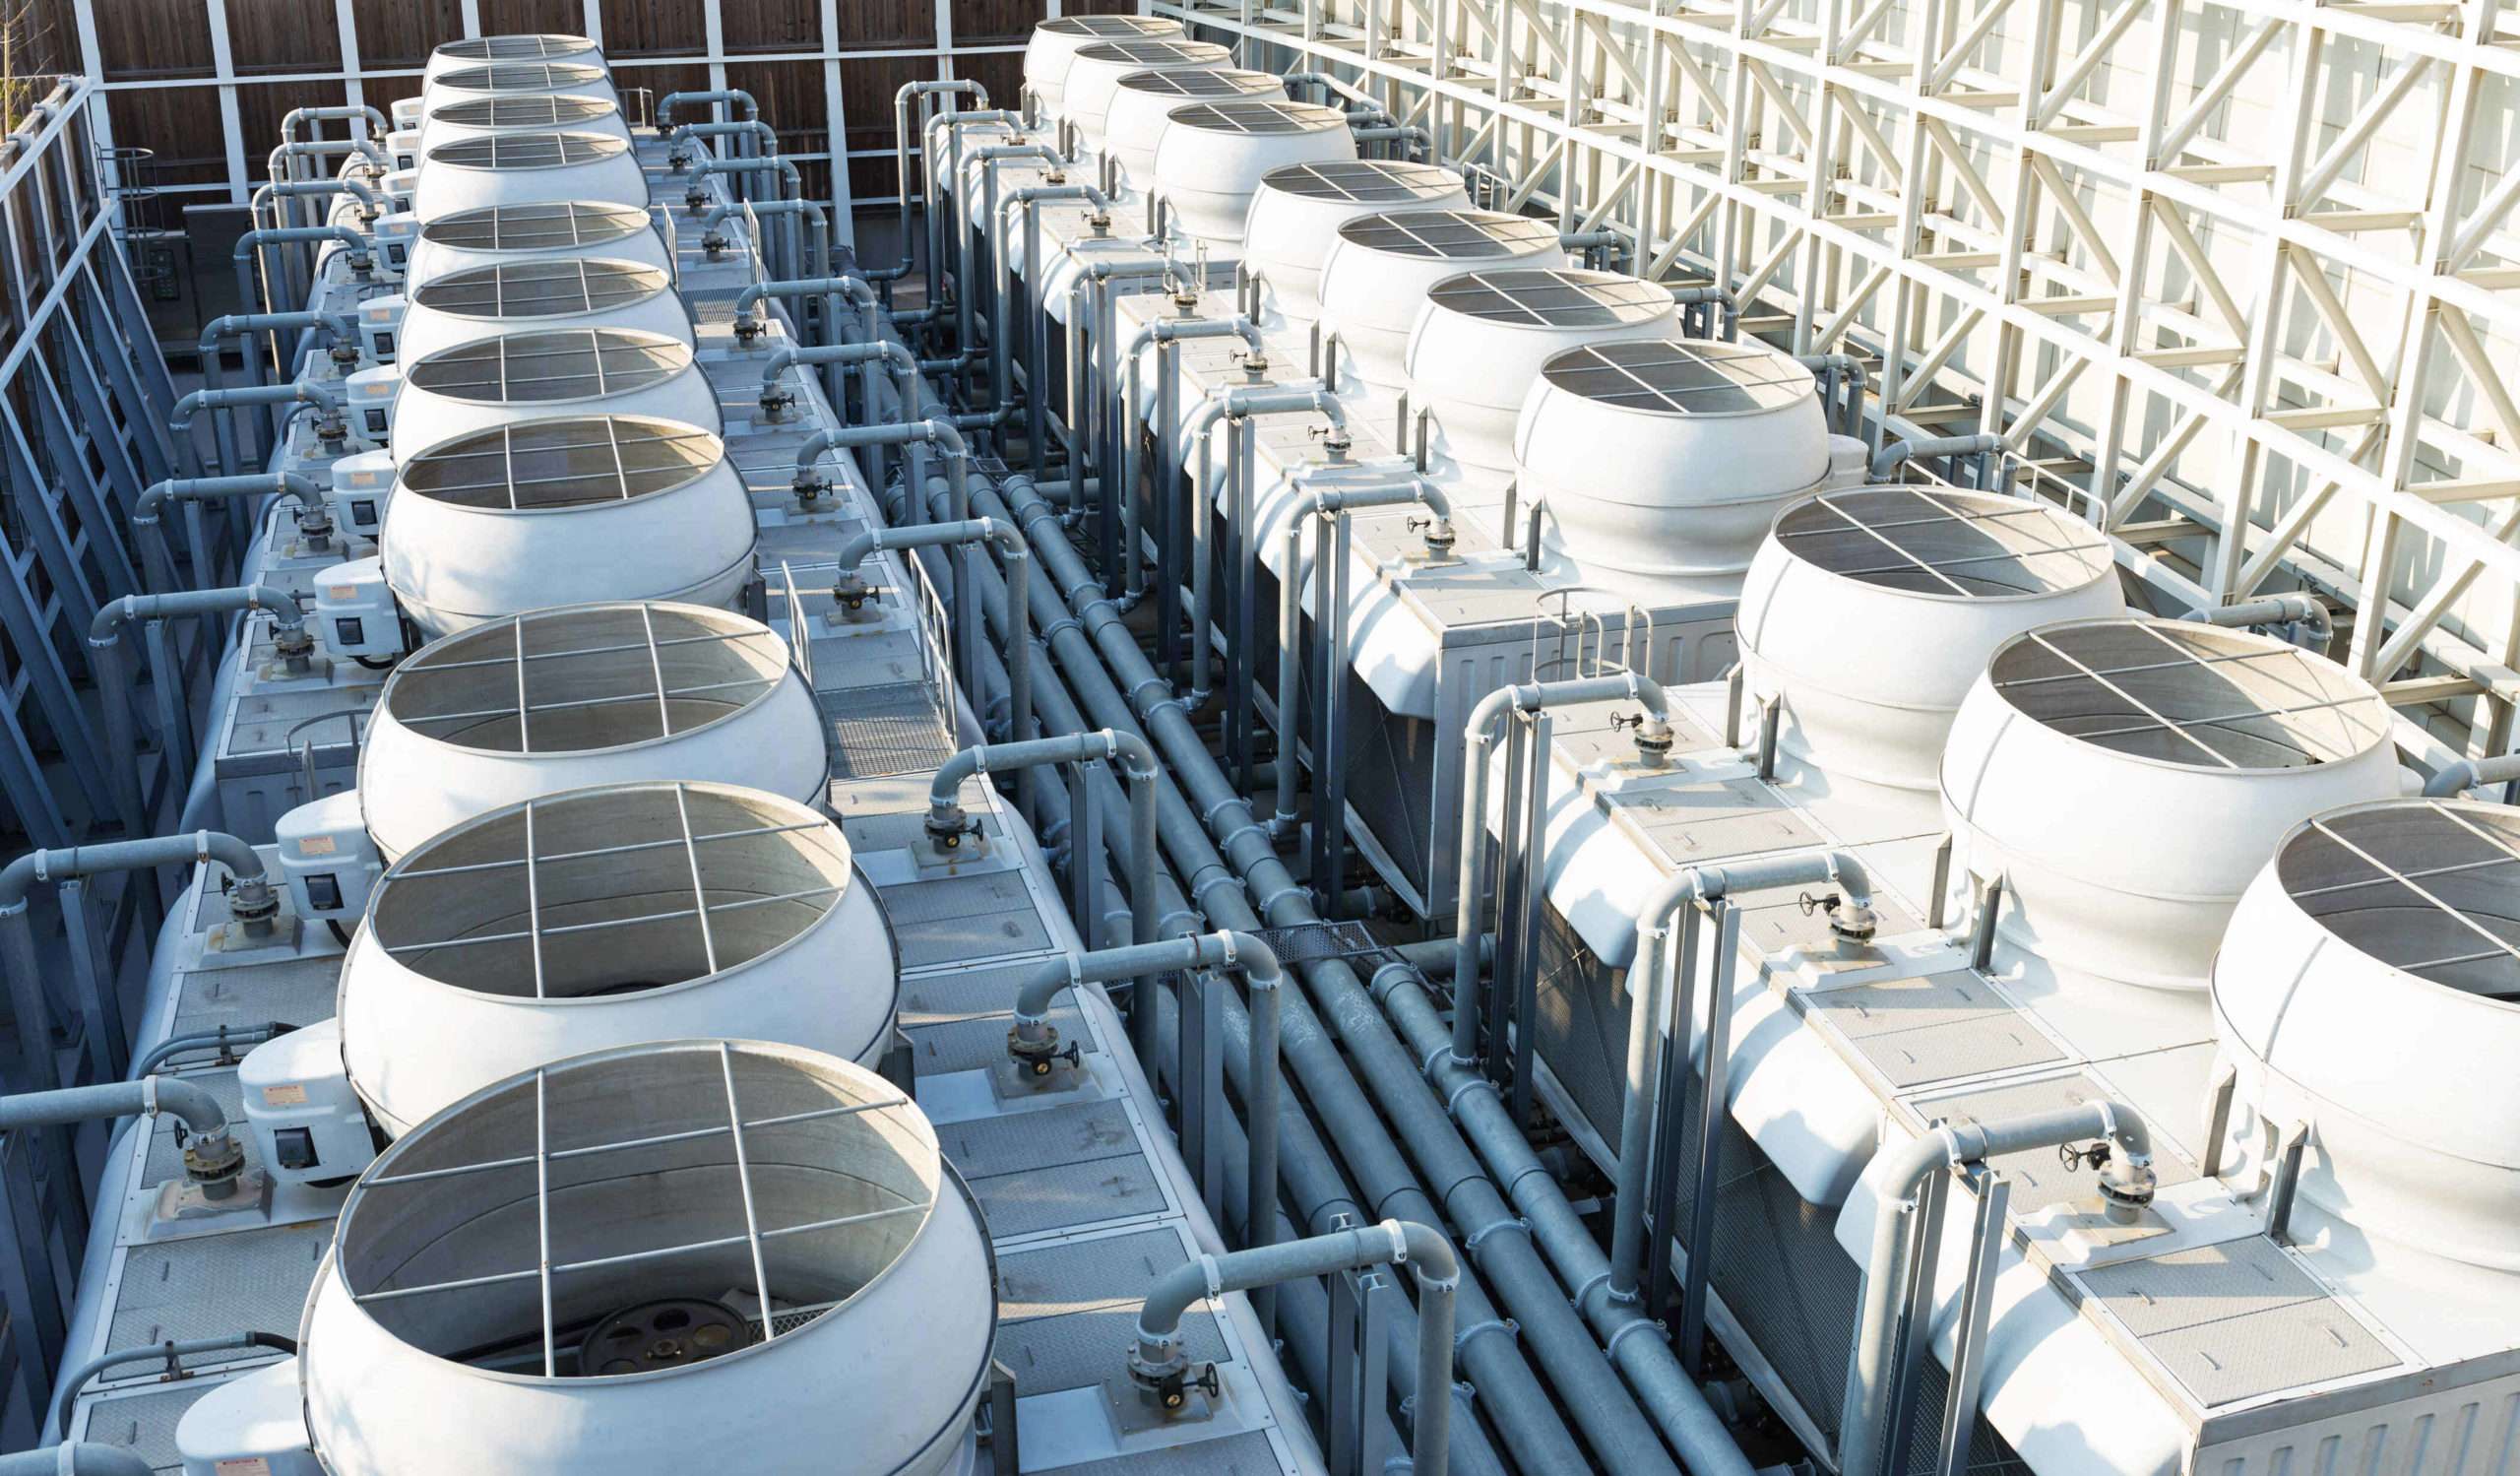
Cooling Tower Water Treatment using scale and corrosion inhibitors, oxidizing and non-oxidizing biocides, pH adjusters, and dispersants to control mineral deposits, biological growth, and maintain heat transfer efficiency.
Both applications benefit from automated, flow-paced chemical metering that adjusts to load changes and operating conditions.
Why Precision Matters
Let's
Optimize Your Program
Protect your boilers and cooling systems from corrosion, scale, and microbiological risk. Let Blue-White® help you select the right chemical metering pump, flow meter, or integrated feed system for your application.
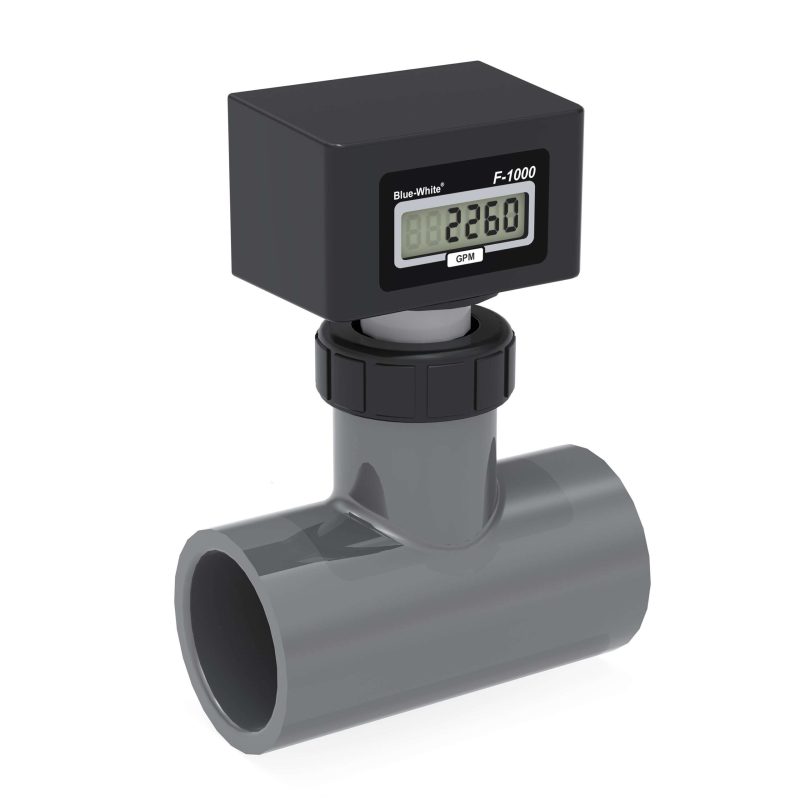
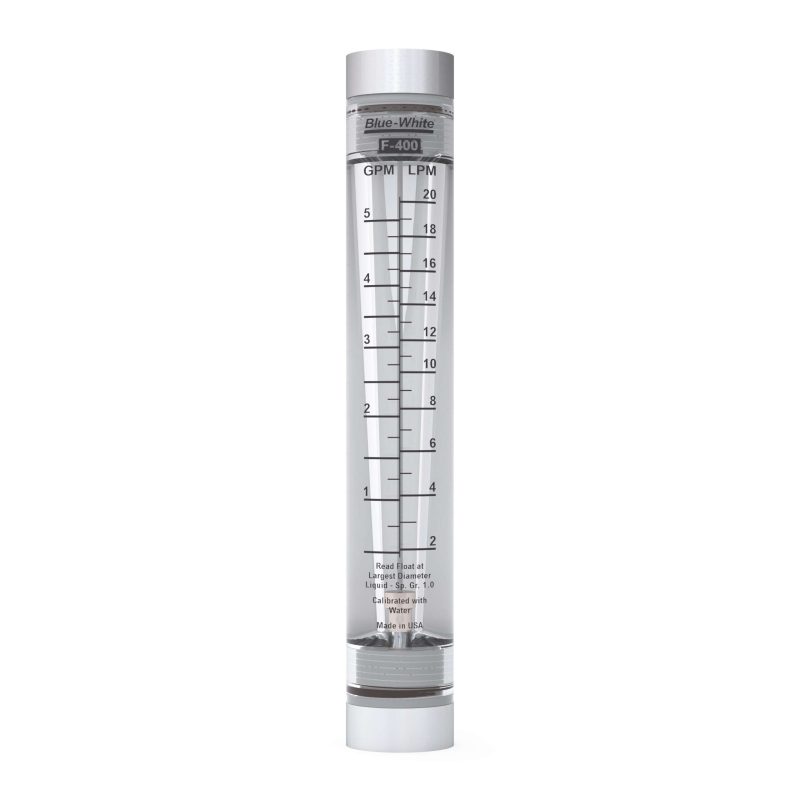
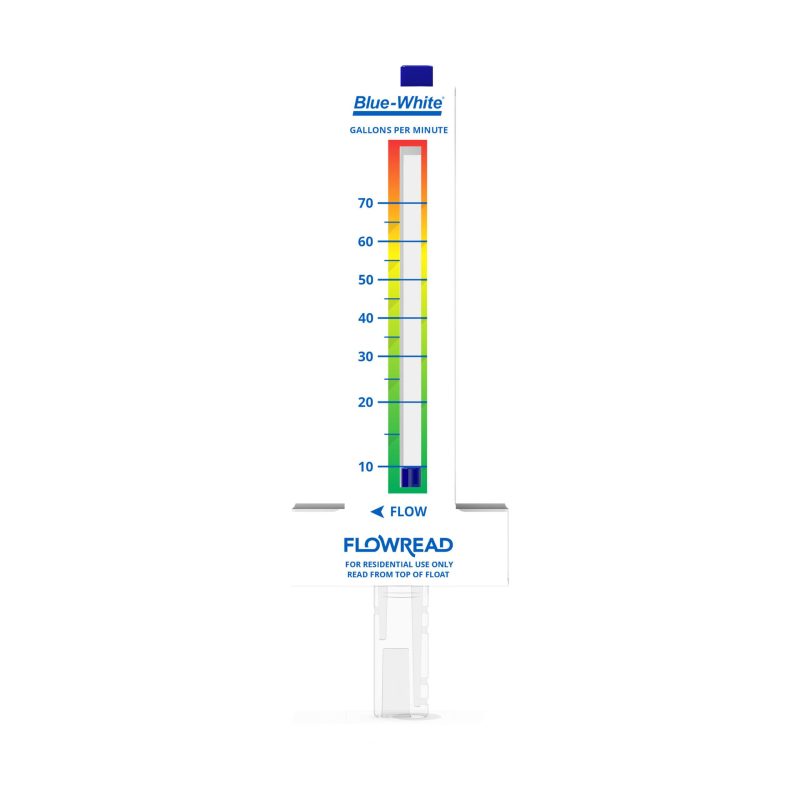
Blue-White® delivers peristaltic and diaphragm metering pumps, industrial flow meters, and customizable chemical feed skid systems engineered for accurate dosing across a wide range of flows, pressures, and chemical types. Our systems support 4–20 mA control, batch dosing, remote start/stop, and flow verification to maintain tight process control.
Durable NEMA 4X/IP66-rated enclosures, chemical-resistant materials, and service-friendly designs help reduce downtime in demanding mechanical room environments. Whether protecting a high-pressure steam boiler or a multi-cell cooling tower system, Blue-White® provides dependable chemical metering solutions that safeguard efficiency, extend asset life, and support long-term operational performance.
To help us address your inquiry as quickly as possible, please fill out the form below.
We use cookies on our website to give you the most relevant experience by remembering your preferences and repeat visits. By clicking “Accept”, you consent to the use of ALL the cookies.
This website uses cookies to improve your experience while you navigate through the website. Out of these, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may affect your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously.
Cookie
Duration
Description
cookielawinfo-checkbox-advertisement
1 year
Set by the GDPR Cookie Consent plugin, this cookie is used to record the user consent for the cookies in the "Advertisement" category .
cookielawinfo-checkbox-analytics
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics".
cookielawinfo-checkbox-necessary
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary".
CookieLawInfoConsent
1 year
Records the default button state of the corresponding category & the status of CCPA. It works only in coordination with the primary cookie.
elementor
never
This cookie is used by the website. It allows the website owner to implement or change the website's content in real-time.
viewed_cookie_policy
11 months
The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Cookie
Duration
Description
_ga
2 years
The _ga cookie, installed by Google Analytics, calculates visitor, session and campaign data and also keeps track of site usage for the site's analytics report. The cookie stores information anonymously and assigns a randomly generated number to recognize unique visitors.
_gat_gtag_UA_85334924_1
1 minute
Set by Google to distinguish users.
_gid
1 day
Installed by Google Analytics, _gid cookie stores information on how visitors use a website, while also creating an analytics report of the website's performance. Some of the data that are collected include the number of visitors, their source, and the pages they visit anonymously.
CONSENT
2 years
YouTube sets this cookie via embedded youtube-videos and registers anonymous statistical data.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.
Cookie
Duration
Description
VISITOR_INFO1_LIVE
5 months 27 days
A cookie set by YouTube to measure bandwidth that determines whether the user gets the new or old player interface.
YSC
session
YSC cookie is set by Youtube and is used to track the views of embedded videos on Youtube pages.
yt-remote-connected-devices
never
YouTube sets this cookie to store the video preferences of the user using embedded YouTube video.
yt-remote-device-id
never
YouTube sets this cookie to store the video preferences of the user using embedded YouTube video.